切入式滚子凸度超精原理及油石尺寸对超精效果的影响
2020-10-21 03:50:24郭培锐刘旗高武正刘凯歌
科技创新与应用
2020年30期
郭培锐 刘旗 高武正 刘凯歌
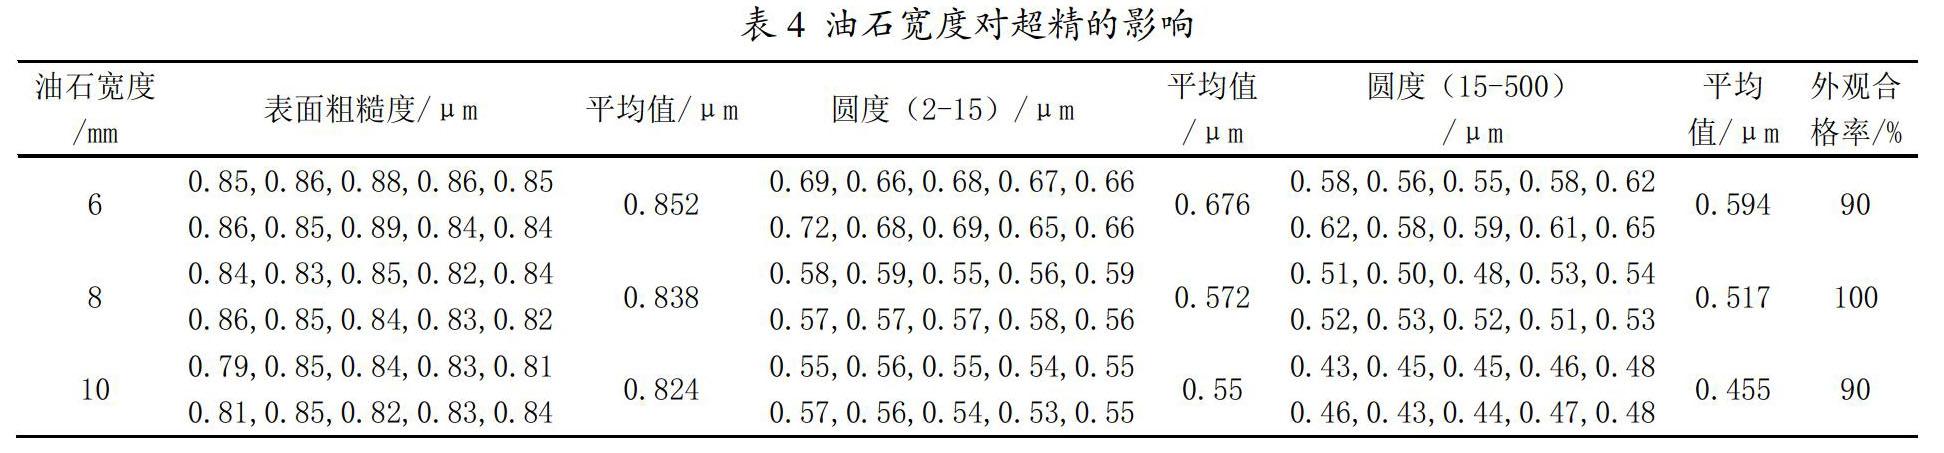
摘 要:通过对SUPFINA公司的切入式滚子超精机Roller Flex 778加工原理及油石夹具的结构分析,在现有两幅油石夹具只能安装宽度为4mm和8mm油石的情况下,设计制作一种辅助工装,保证油石装夹的中心不变,扩展安装更多不同宽度的油石,以满足较大直径滚子超精加工的需求。与此同时,利用窄油石的插补进给工艺参数来验证油石尺寸对超精效果的影响,结果表明:油石宽度影响圆度、波纹度的改善,长度影响母线轮廓成形,高度影响超精稳定性和加工效率。
关键词:切入式滚子超精机;油石夹具;尺寸;凸度;验证
中图分类号:TH133.33 文献标志码:A 文章编号:2095-2945(2020)30-0104-04
Abstract: Through the analysis of the processing principle of the in-feed roller superfinishing machine Roller Flex 778 and the structure of the oilstone clamp of SUPFINA Company, in the case that the existing two oilstone clamps can only install 4mm and 8mm oilstone, this paper designs and makes a kind of auxiliary tooling to ensure that the center of the oilstone clamping remains unchanged and expand the installation of more oilstones of different widths to meet the needs of superfinishing of larger diameter rollers. At the same time, the interpolation feed process parameters of narrow oilstone are used to verify the effect of oilstone size on ultra-precision effect. The results show that the width of oilstone affects the improvement of roundness and waviness, and the length affects the forming of busbar contour, its height affects super-precision stability and processing efficiency.
Keywords: in-feed roller superfinishing machine; oilstone clamp; size; convexity; verification
超精研是滚子加工过程的最后一道工序,尤为关键。目前,滚子超精研的方式有两种:切入式、贯穿式[1]。贯穿式是主要的,生产效率高,更适合大批量的普通精度产品,但导辊加工难度大,特别是圆锥滚子的对数曲线修形;切入式工装相对简单、易于调整、技术准备周期短,有较强的工艺性,但对设备各运动轴精度、同步控制精度以及油石装夹工装要求高。
1 切入式滚子超精机
1.1 设备配置
图1为SUPFINA公司生产的切入式滚子超精机加工部位示意图,其基本特征是:滚子外径依靠匹配的导辊实现外径定位和驱动,大小端面依靠支承块实现轴向定位。
设备配置为双工位多工步循环,每个工位的超精单元均配置水平数控轴X、垂直数控轴Y、旋转数控轴C以及一个直线振荡器;支承辊驱动、振荡频率、振荡冲程、叠加冲程及油石夹具的旋转角度(一定范围内)均可实现无级可变[2]。……
登录APP查看全文